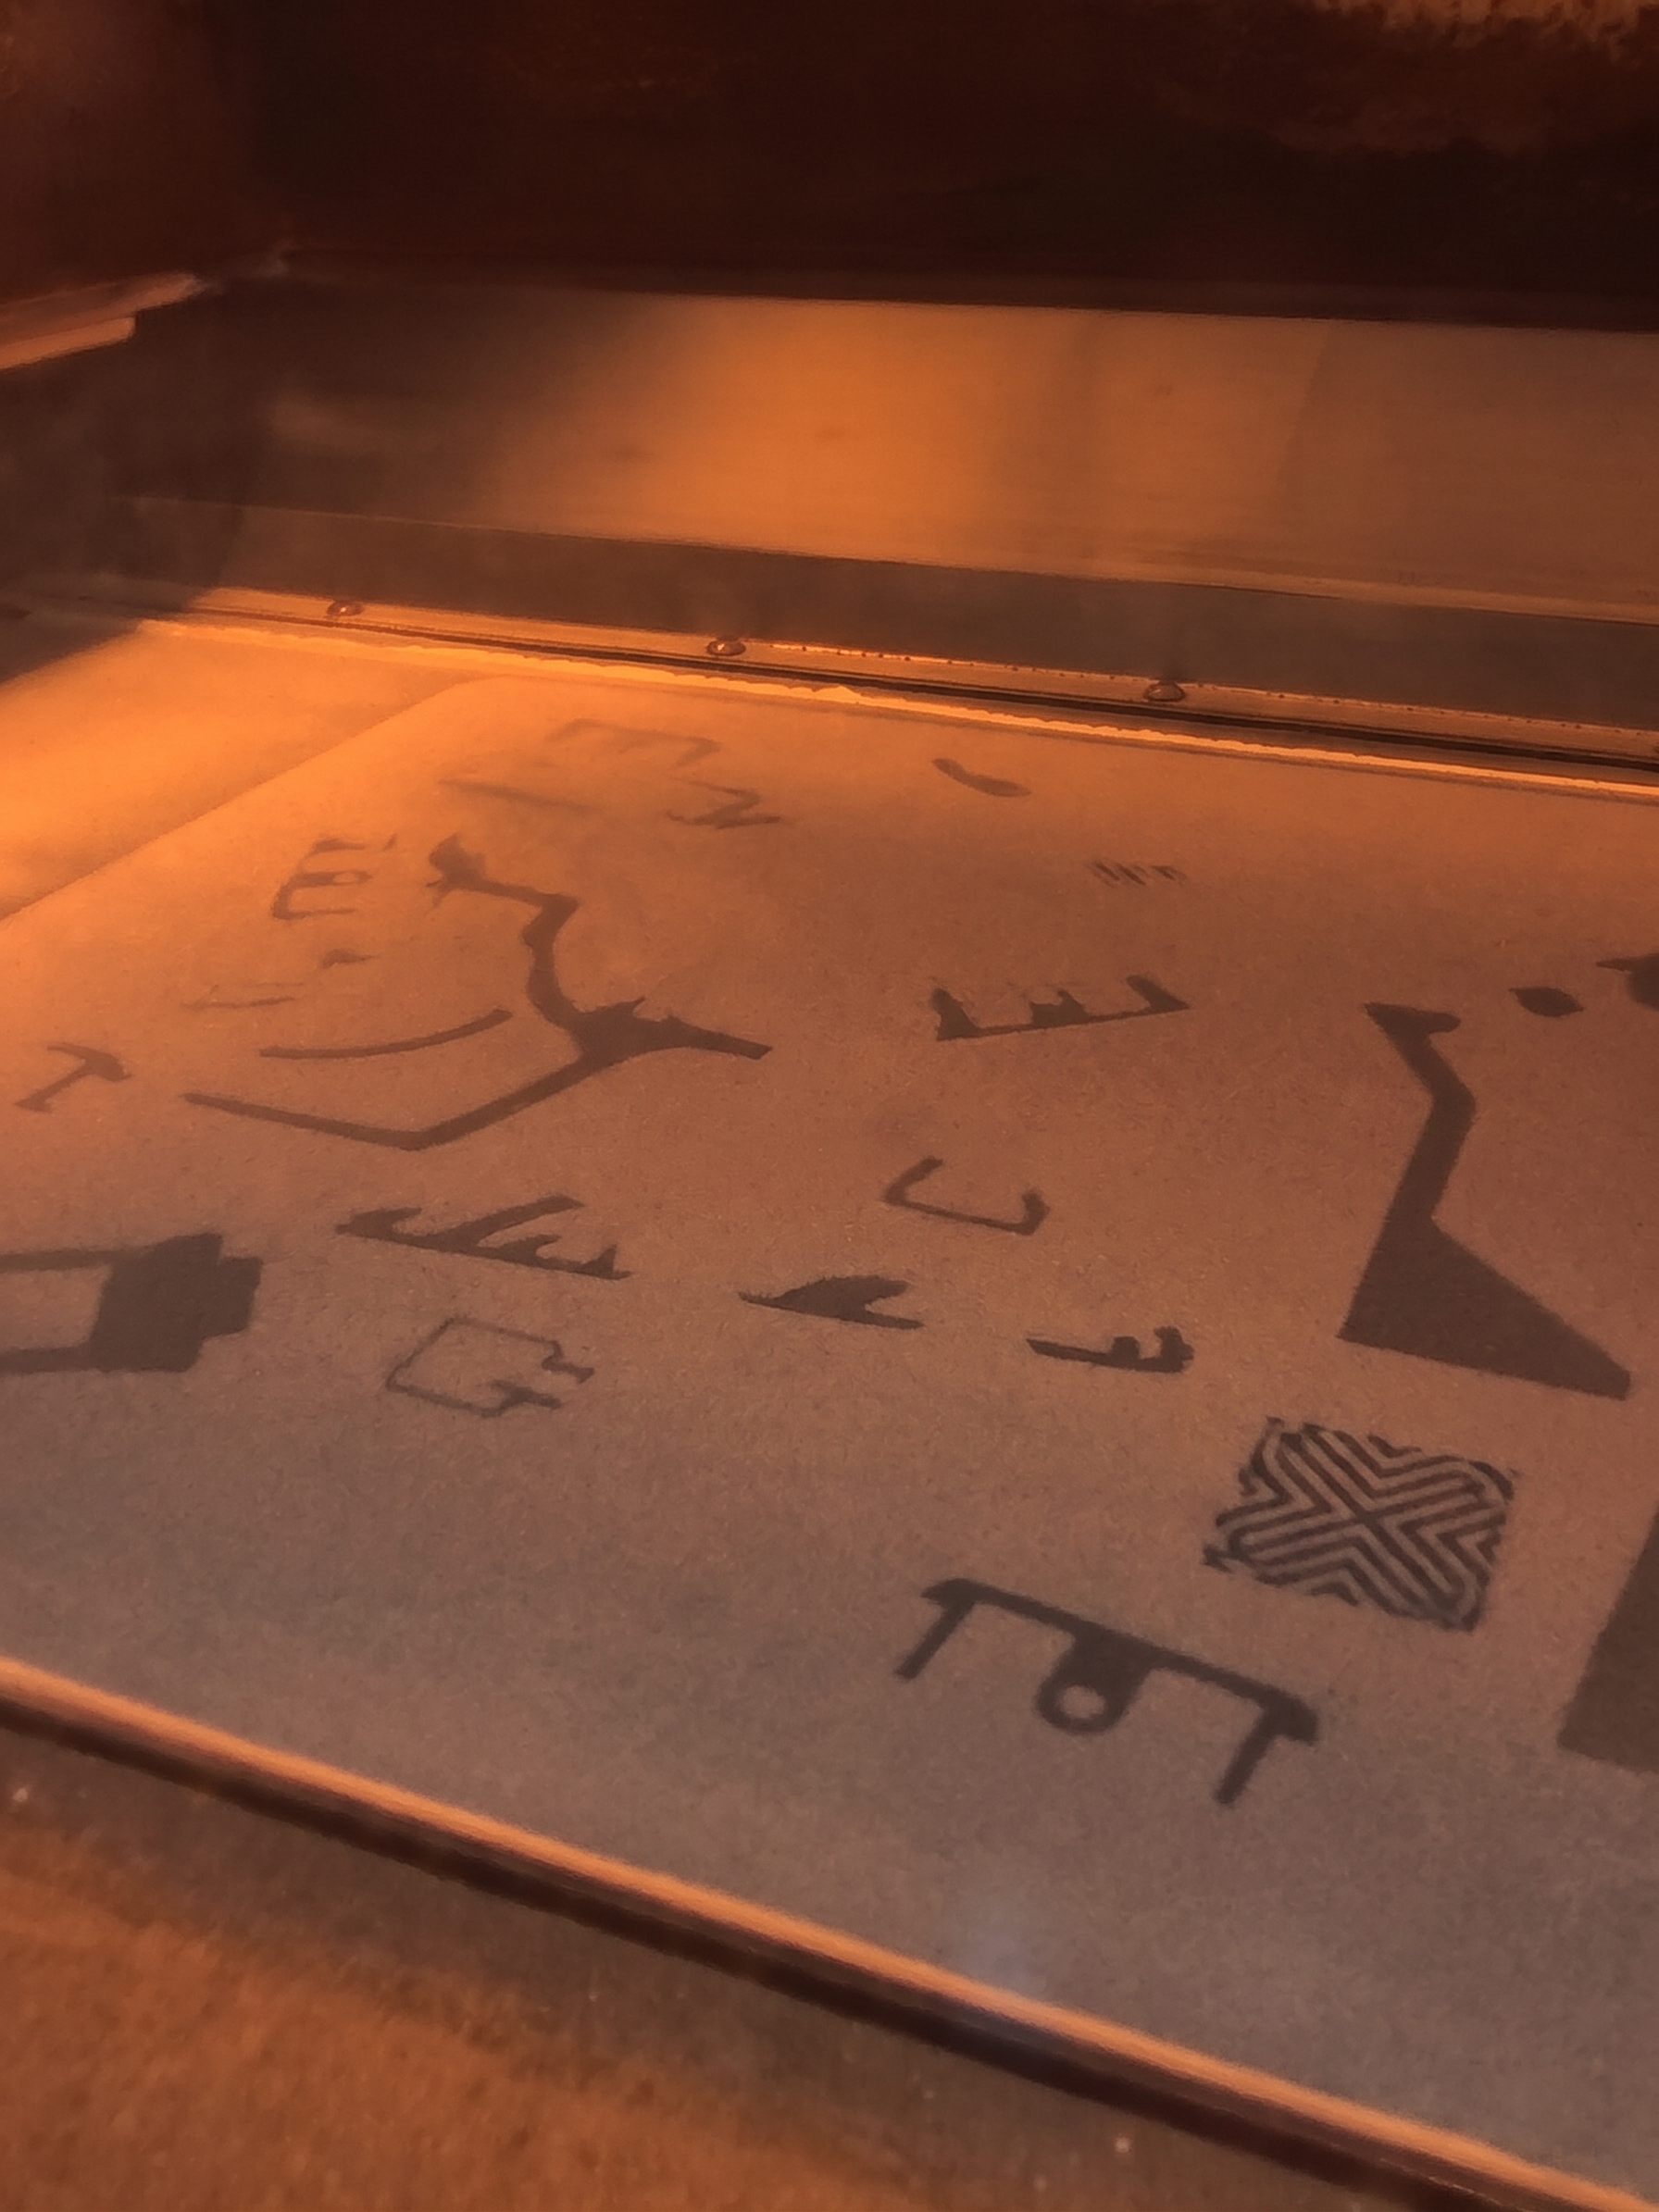
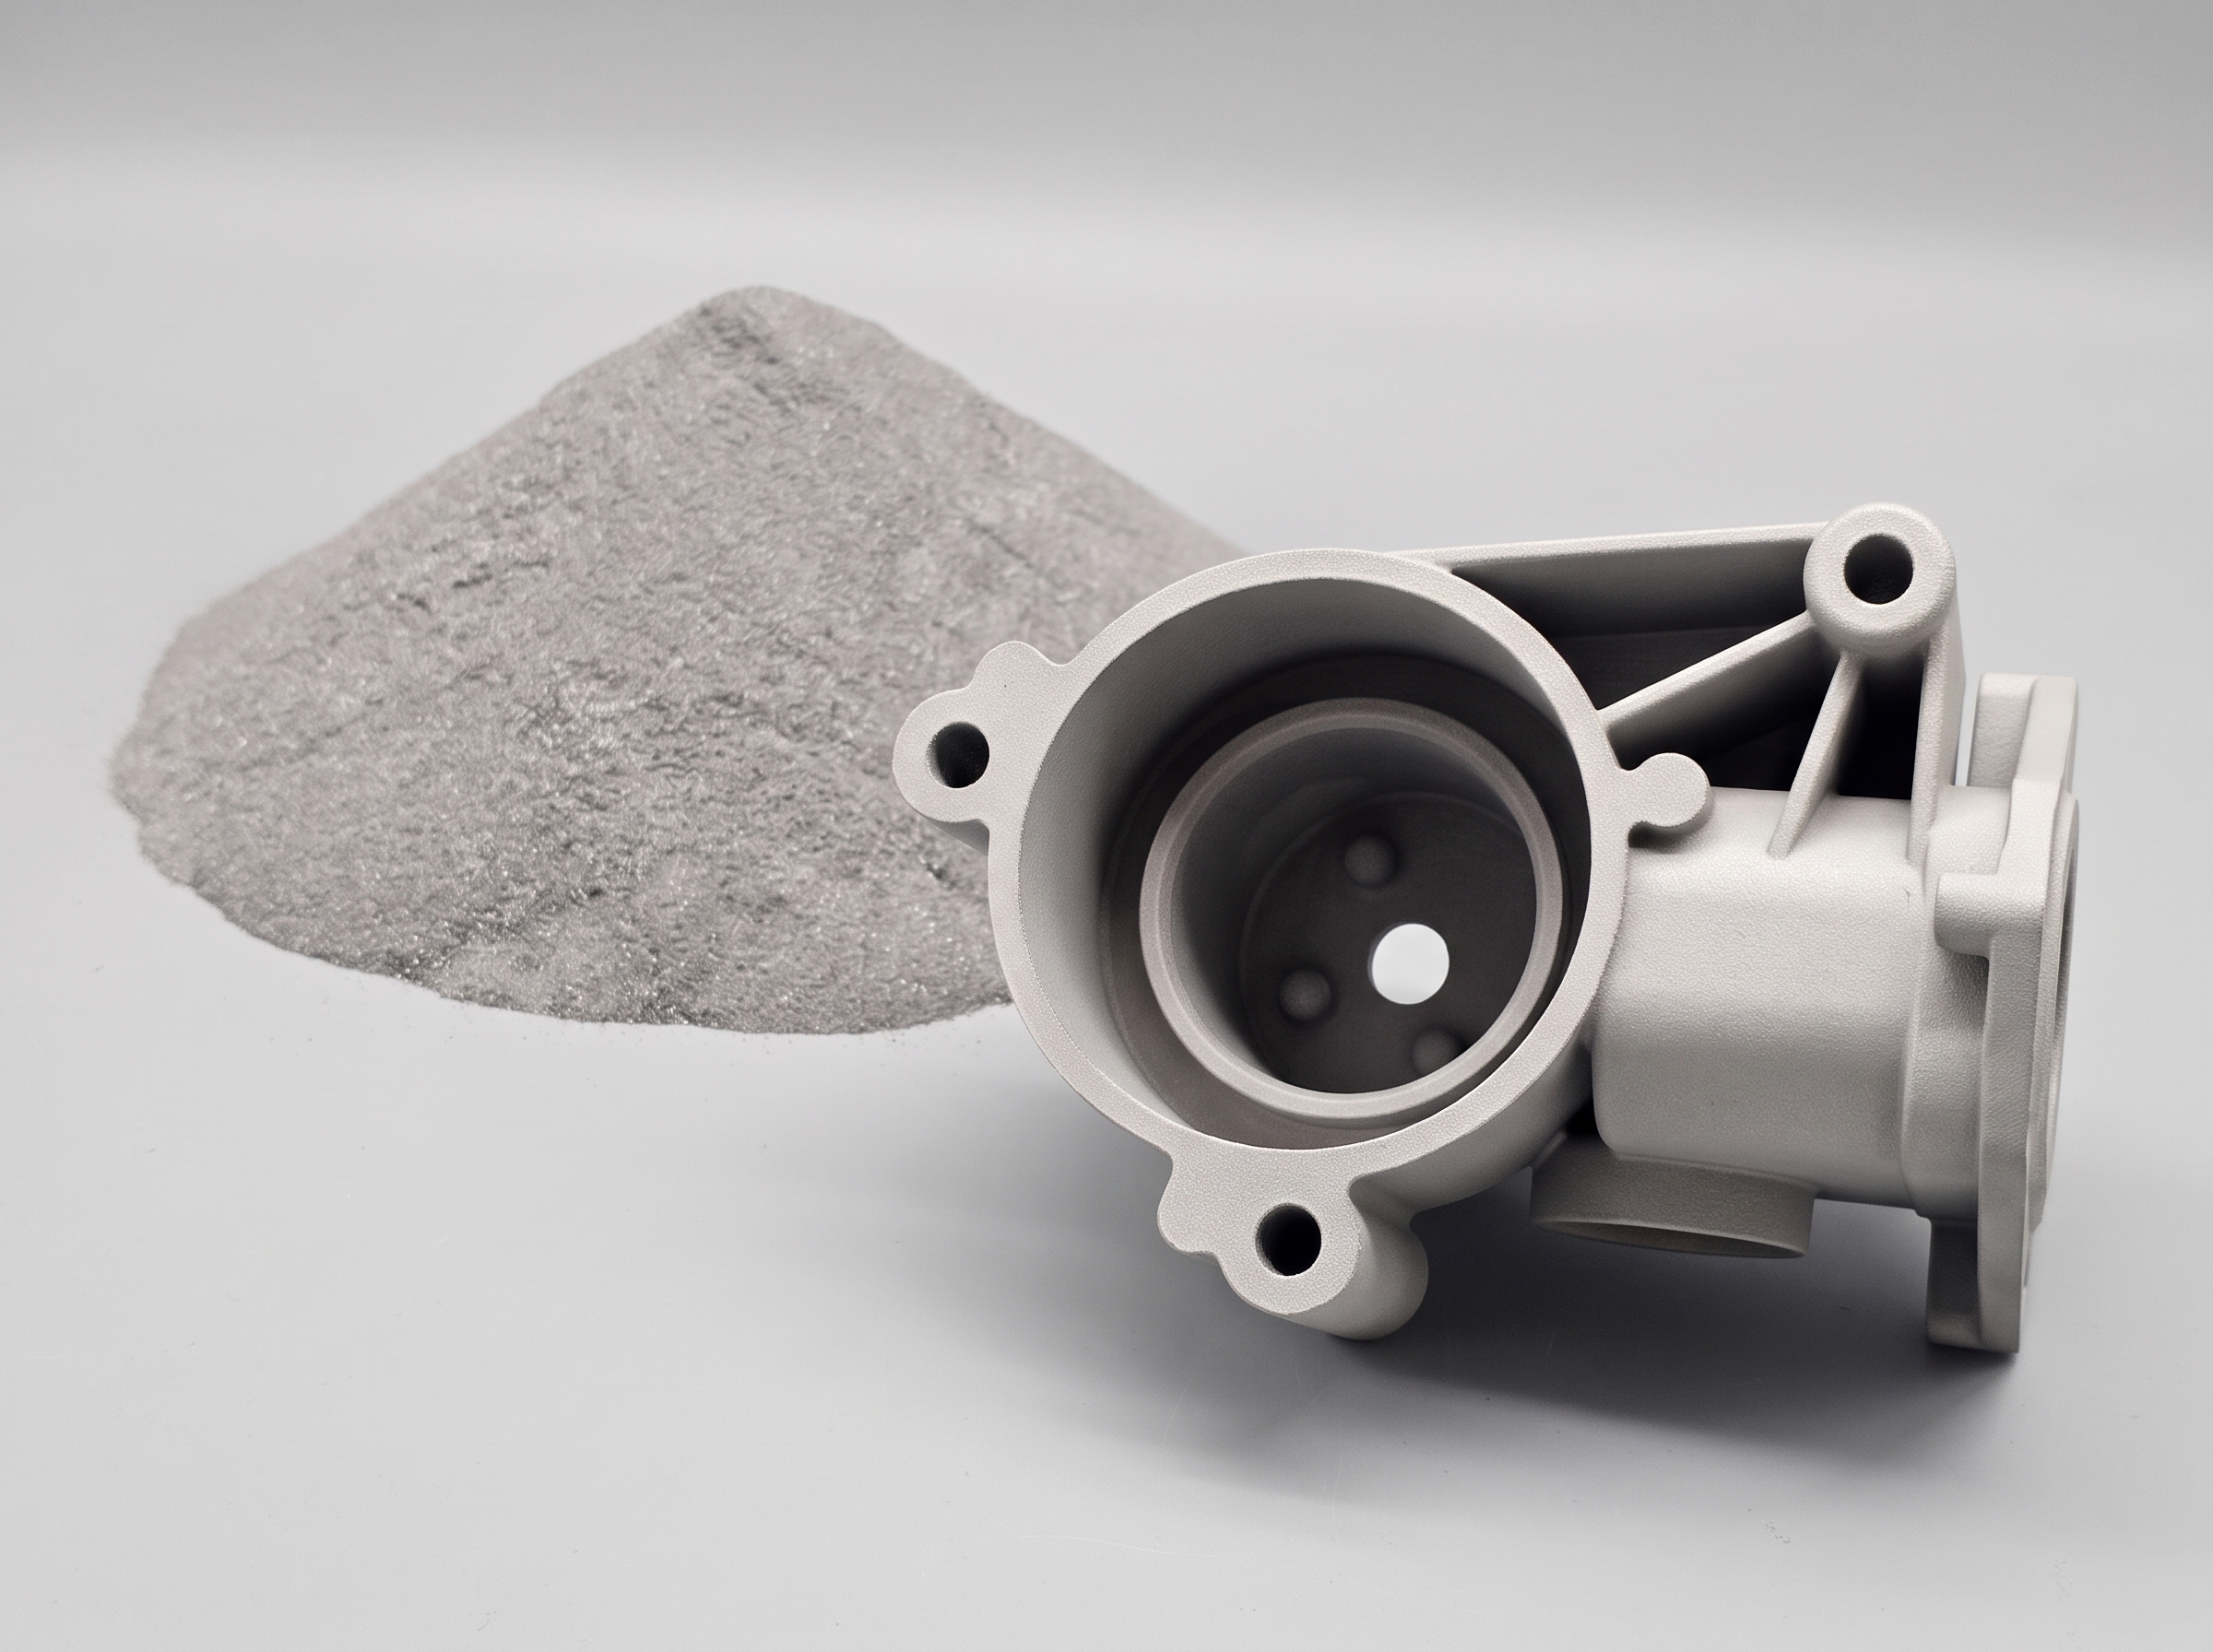
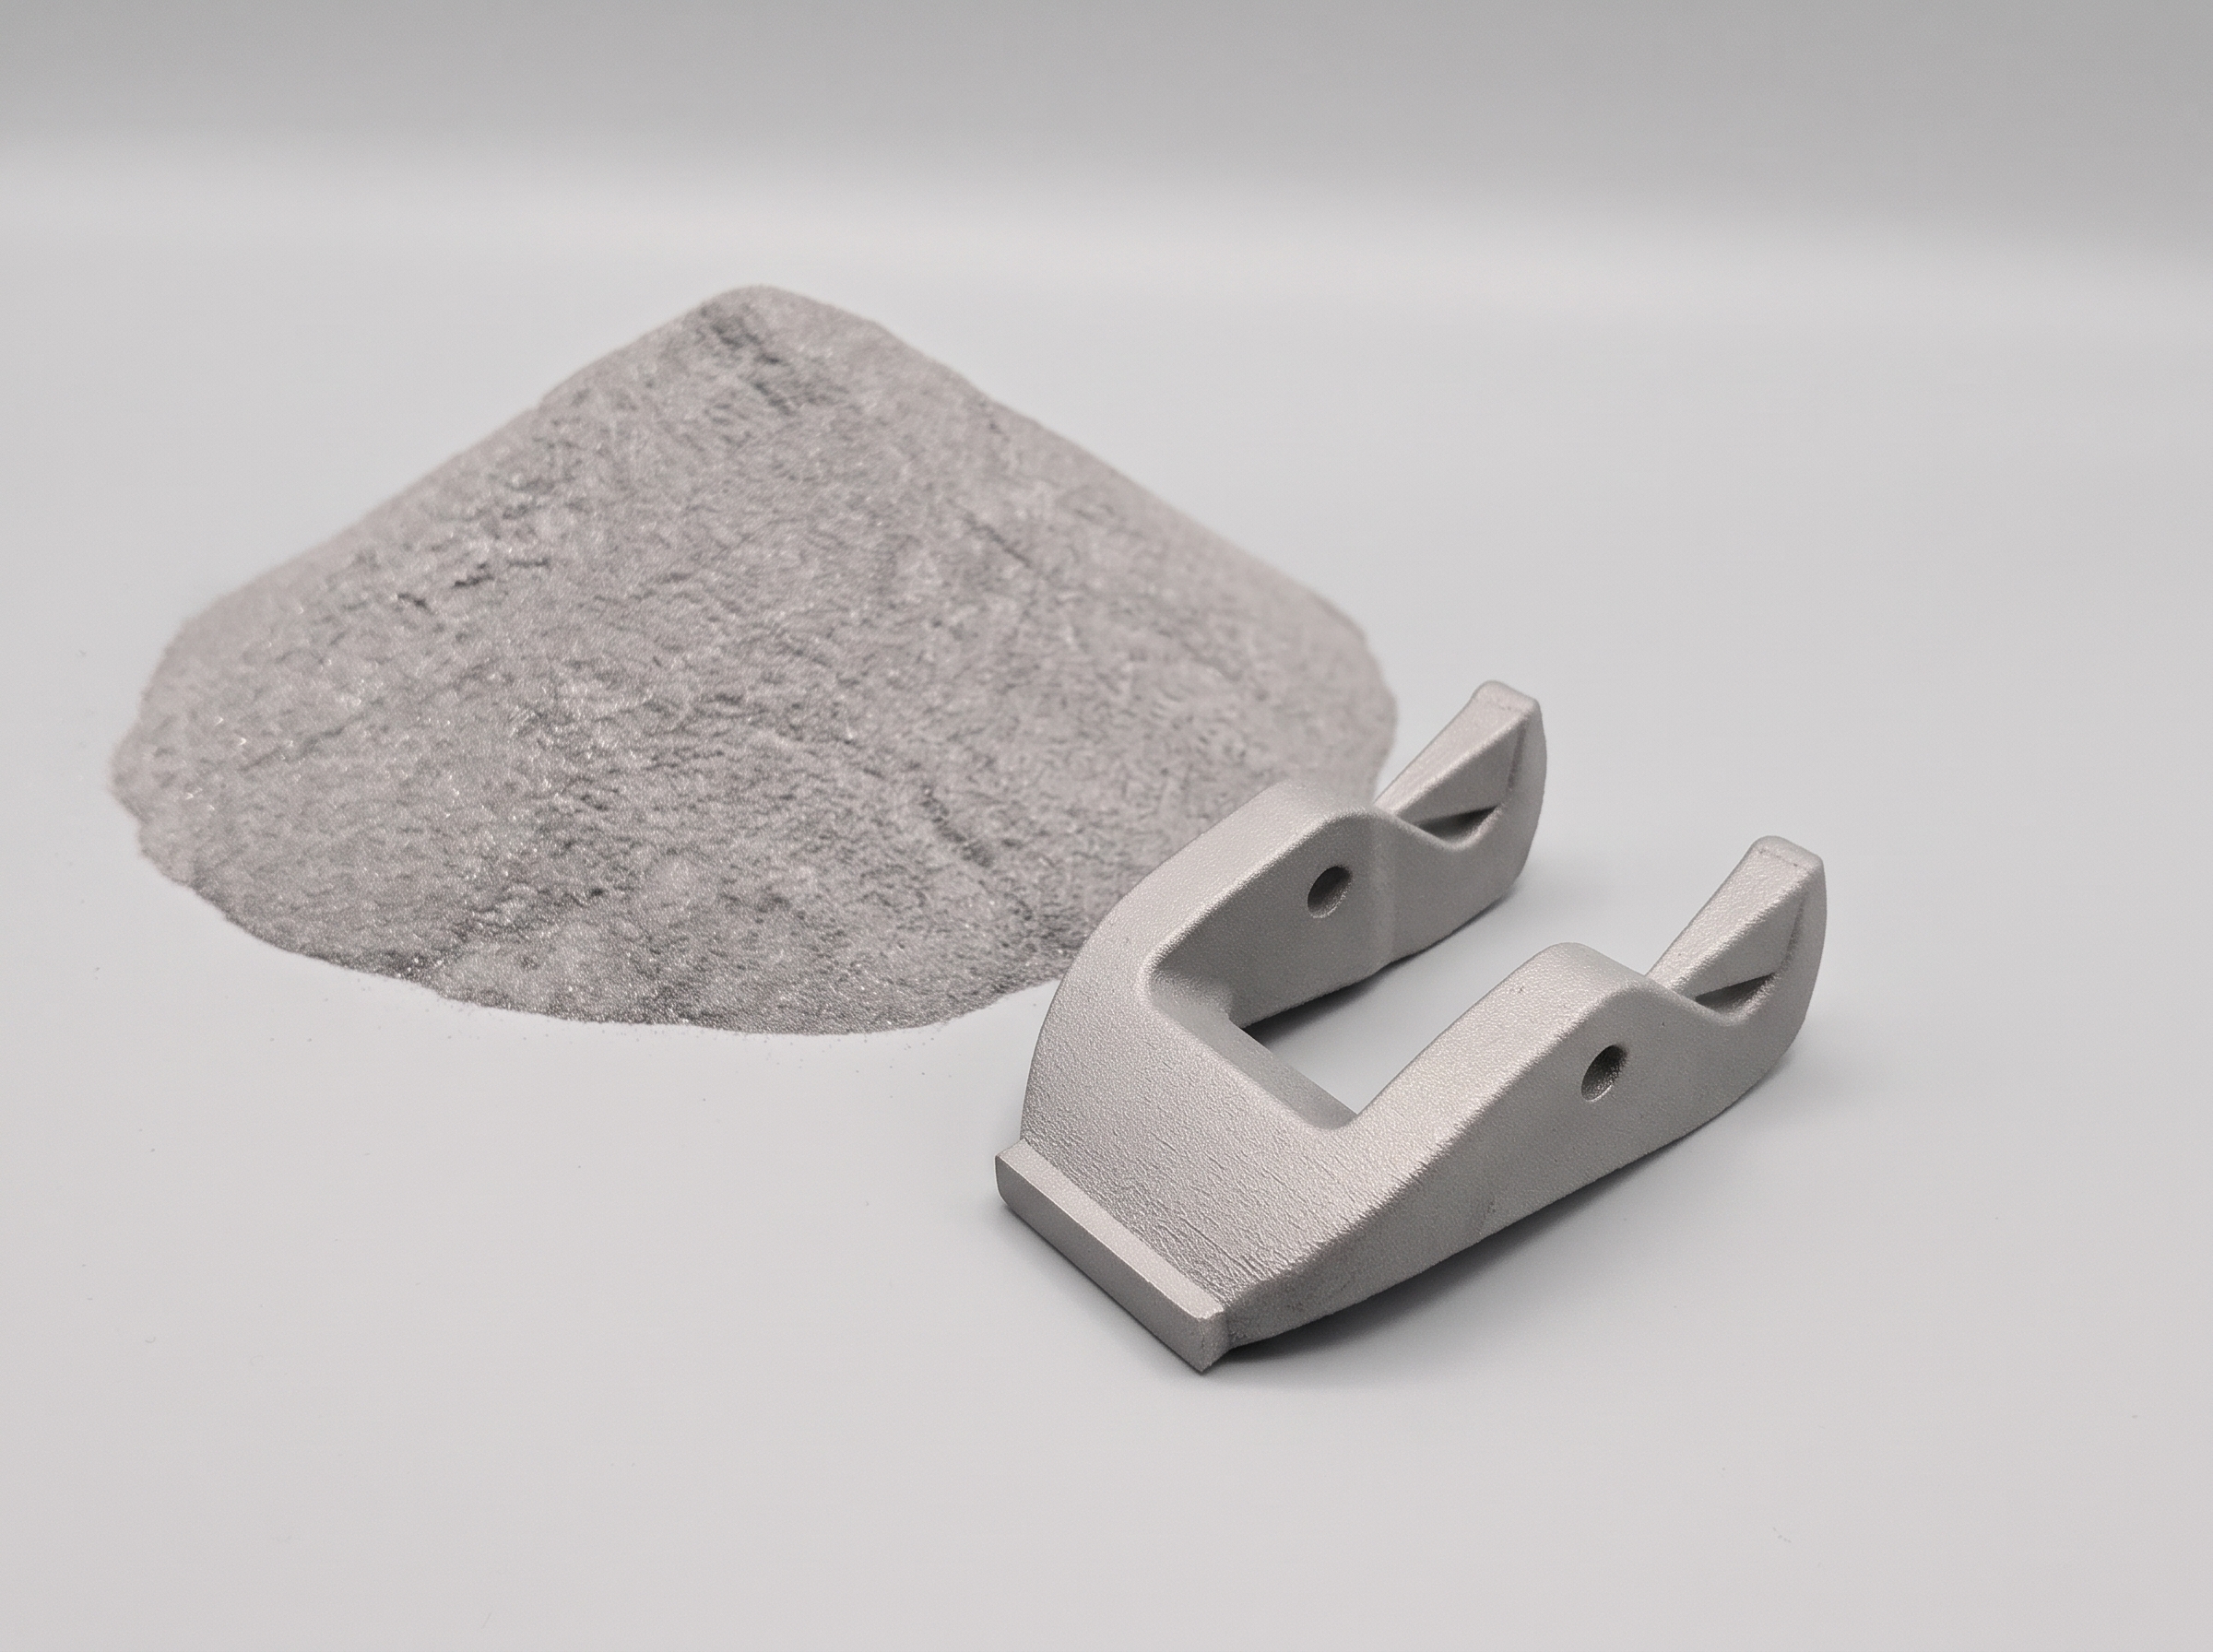

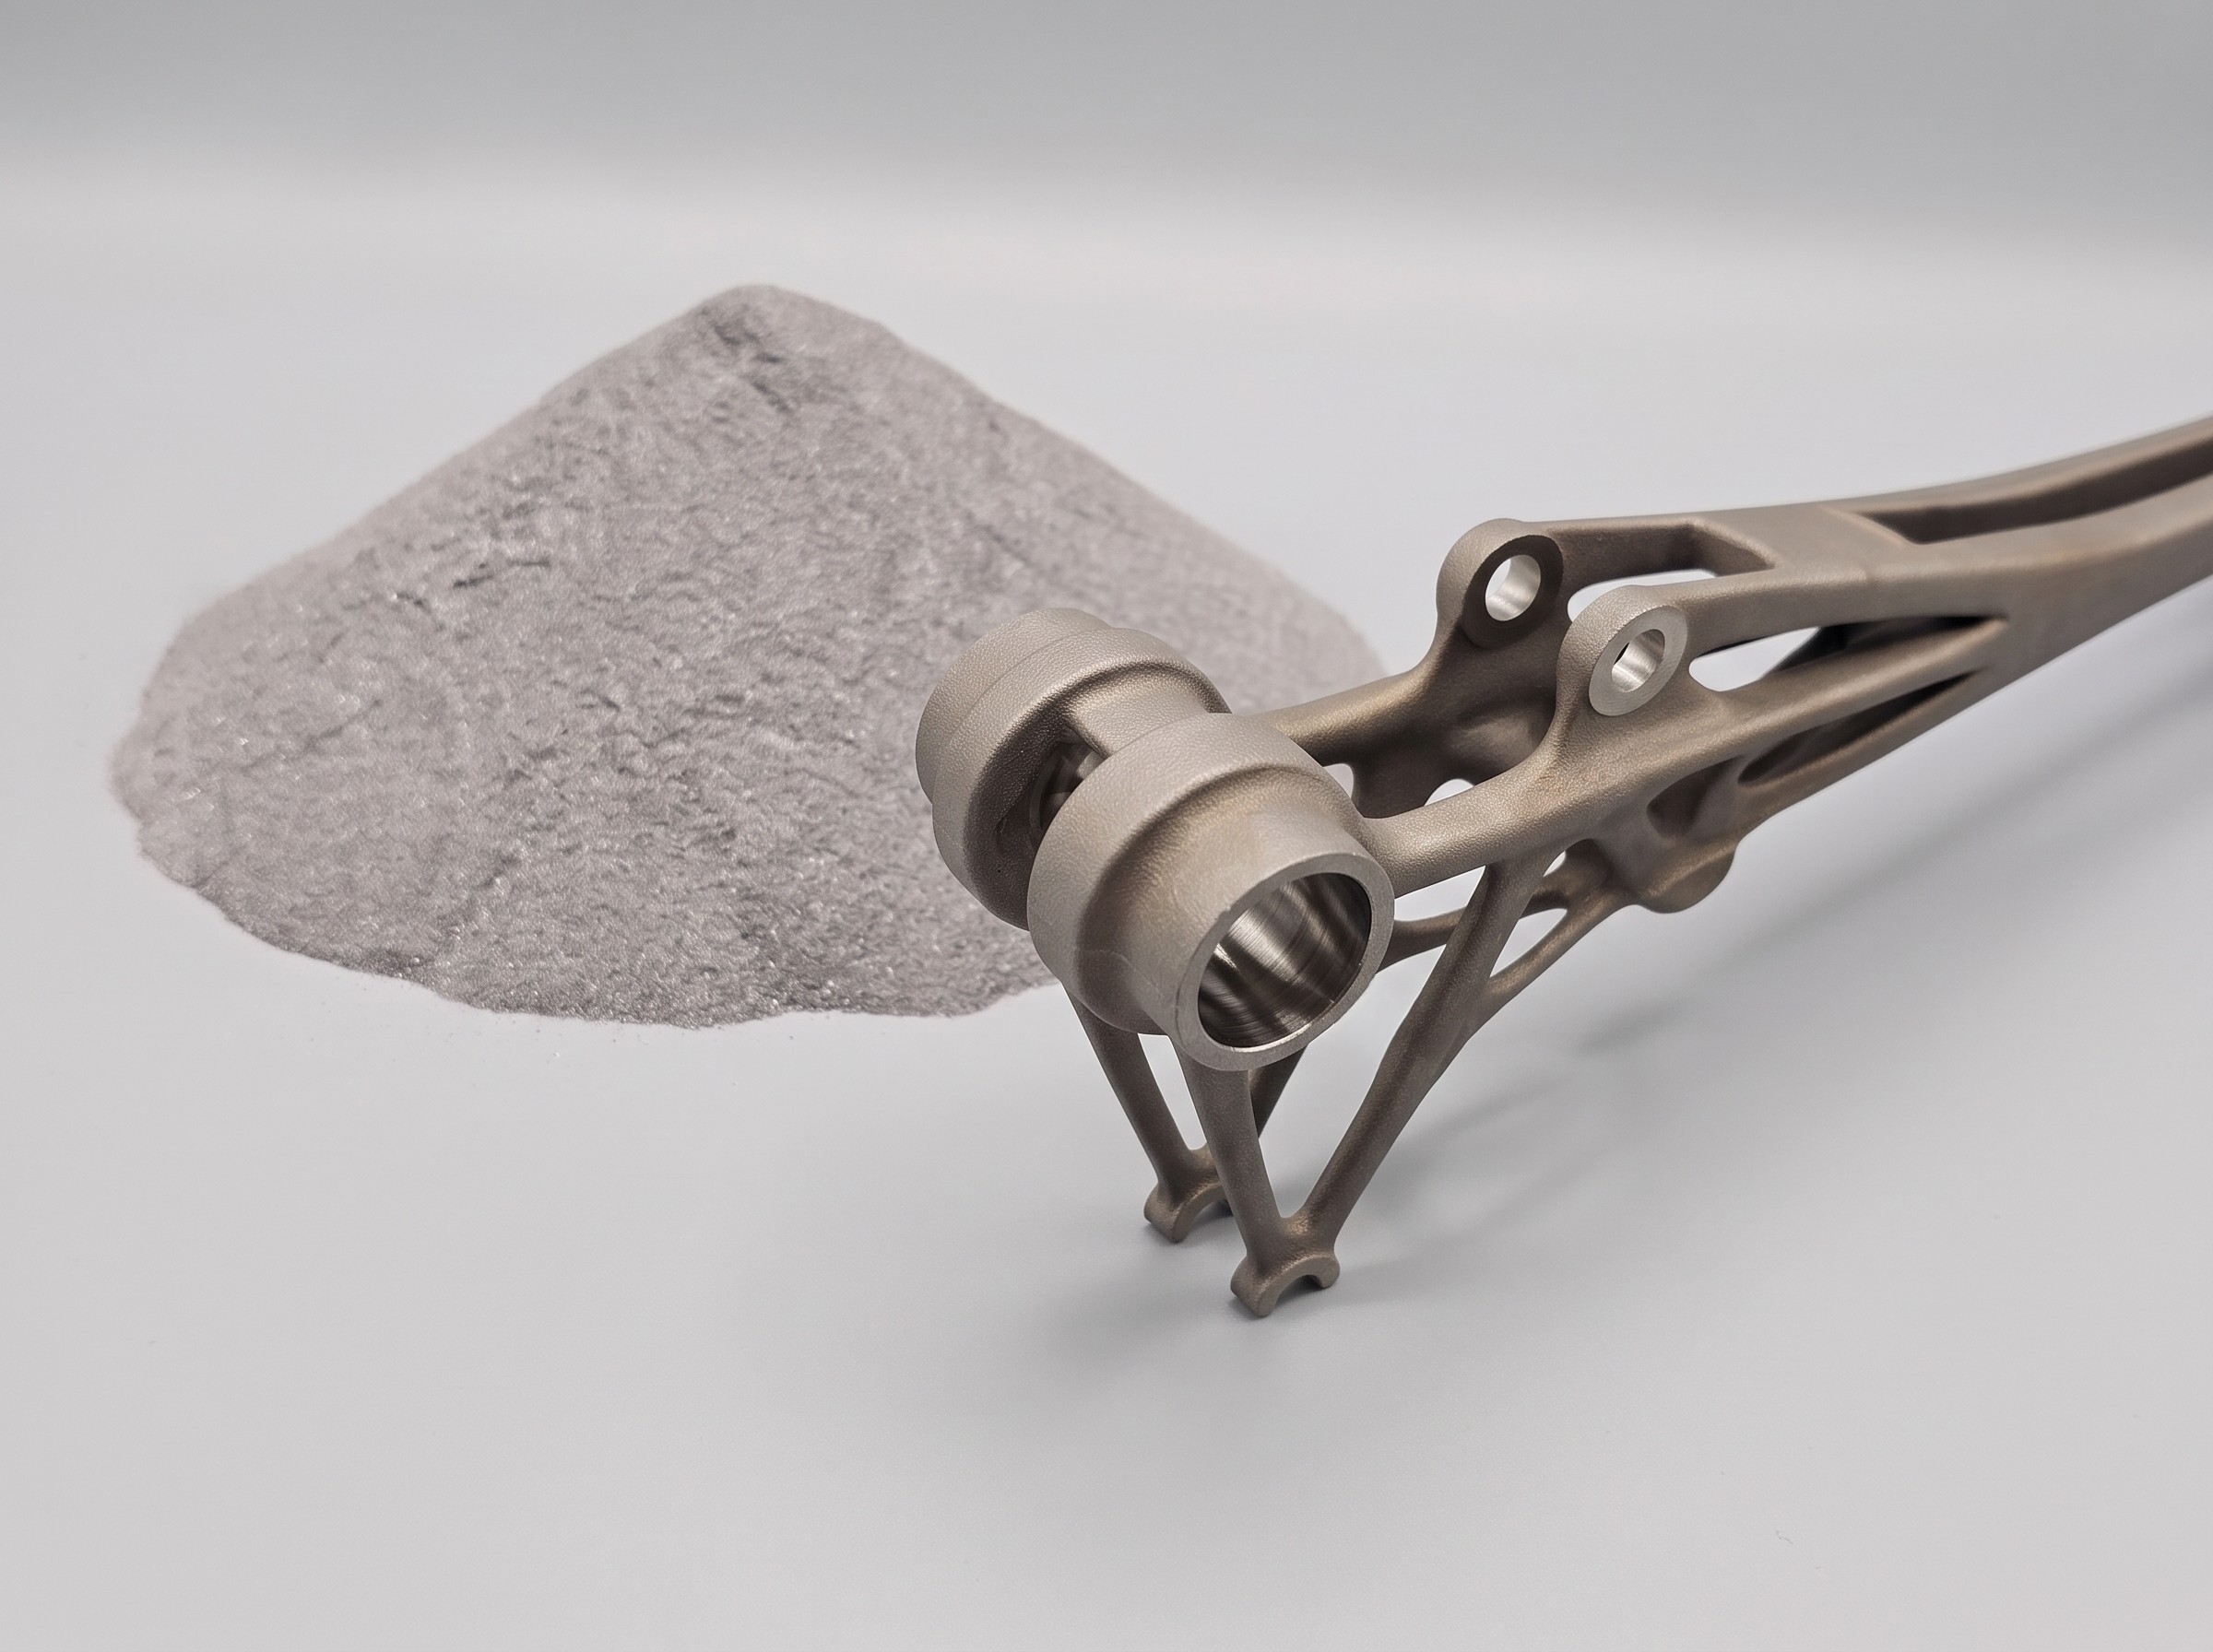

In Selective Laser Melting (SLM), fine metal powder is fully melted under high-purity argon or nitrogen shielding gas in ultra-thin layers of 0.02 to 0.06 mm. This achieves a part density exceeding 99.9 %. Mechanical strength values match wrought bar stock and significantly outperform conventional metal castings in both ductility and pore-free integrity.
Printing aluminum and steel in the same machine risks foreign particle inclusions and brittle parts. That is why production is carried out on strictly segregated, material-dedicated systems for each alloy family: separate setups for stainless steels (AISI 316L / 1.4404 and precipitation-hardening 17-4 PH / 1.4542), lightweight aluminum (AlSi10Mg), titanium (Ti6Al4V), and weldable structural steels (S480 & S700). This guarantees 0 % cross-contamination and 100 % alloy purity.
Yes. Whenever technically required, SLM metal parts undergo thermal stress-relief annealing in a furnace before being precisely cut from the build plate via wire EDM or band saw. All support structures are then mechanically removed and the surface is media-blasted for a clean, matte-metallic finish. Upon request, targeted precipitation hardening (e.g., for 17-4 PH) and CNC post-machining for tight fits and sealing surfaces are included right out of the box.
Modern SLM systems easily accommodate a single-piece build volume of up to 280 x 280 x 350 mm. Even larger metal structures can be reliably manufactured as multi-part assemblies and welded together thanks to the excellent weldability of the printing alloys (especially 316L stainless steel, AlSi10Mg aluminum, and S480 / S700 structural steels).